Mold Project Checklist 101: Manufacturing Communication for Commercial Plastic Assemblies
A molded part project becomes predictable when the mold, resin, inspection plan and shipping expectation are discussed before steel is cut. This article uses a commercial plastic assemblies scenario, 9 checkpoints and a simple capacity calculation to show how a buyer can review a China-based mold partner without relying on guesswork.
Key takeaways
- Plan the first review around 9 named checkpoints, not a single final shipment date.
- Use ±0.01 mm as a discussion point only when the drawing marks the critical feature and the inspection method.
- A 2-cavity or multi-cavity tool should be sized around annual volume, resin behavior and cycle expectations.
- Bridge volumes near 2375 parts still need real resin trials when assembly fit matters.
Start with the risk that can be measured
The fixture note for this job should record who approved the dimension, which press condition was used, and what changed after trial samples. That sequence is practical because each step creates evidence: marked design notes, steel choices, mold trial sampling records, sample photos and dimensional reports. That small documentation habit can prevent a drawing issue from turning into a production delay.
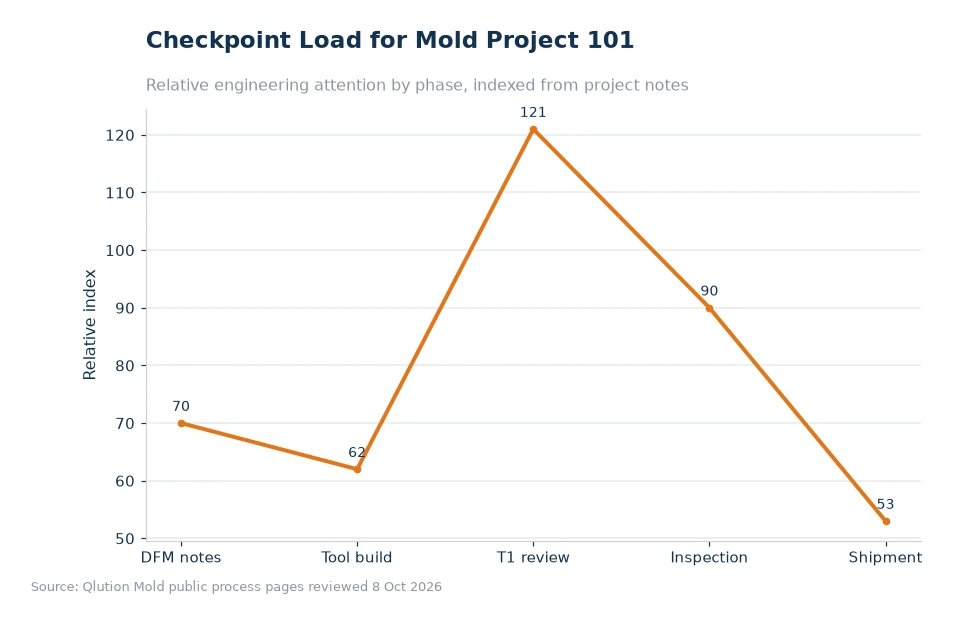
A useful manufacturing communication review begins when the team links the CAD model, target resin and inspection method in one short decision trail. When the buyer asks for a clear acceptance standard, the supplier can compare critical dimensions, visible surfaces, mating features and packaging needs before release. If a T1 sample needs correction, the recorded cause is easier to separate from a new design change.
In the supplier shortlist, Prototype mold manufacturer can be evaluated through the same practical lens: does the team explain DFM findings, mold design choices, trial results and delivery documentation in a way that a remote engineering buyer can verify?
Translate the drawing into process questions
A useful manufacturing communication review begins when the team links the CAD model, target resin and inspection method in one short decision trail. The same discipline also helps overseas communication because English-speaking project engineers can report progress without asking the buyer to interpret shop-floor shorthand. For teams managing cost and timing, this keeps the discussion on measurable risk instead of broad sales language.
The shrinkage card for this job should record who approved the dimension, which press condition was used, and what changed after trial samples. Qlution Mold describes a workflow that moves through file review, DFM and quotation, mold design, tool manufacturing, mold trial and final delivery. If a T1 sample needs correction, the recorded cause is easier to separate from a new design change.
Using PC changes shrinkage, gate freeze and appearance behavior, so the quote should not be separated from the process window. The same discipline also helps overseas communication because English-speaking project engineers can report progress without asking the buyer to interpret shop-floor shorthand. If a T1 sample needs correction, the recorded cause is easier to separate from a new design change.
| Checkpoint | Typical timing | Primary owner | Evidence to request |
|---|---|---|---|
| DFM and quote | 4 working days | engineer | marked CAD notes |
| Mold design approval | 4 working days | tool designer | 2D/3D mold layout |
| Tool manufacturing | 16 working days | toolmaker | machining log |
| T1 sampling | 5 working days | quality team | CMM report |
| Production delivery | 6 working days | project manager | packing checklist |
Use official capabilities as sourcing evidence
For this commercial plastic assemblies case, the planning file should treat draft angle clearance as an engineering item rather than a late cosmetic comment. That sequence is practical because each step creates evidence: marked design notes, steel choices, wire cutting records, sample photos and dimensional reports. If a T1 sample needs correction, the recorded cause is easier to separate from a new design change.
A useful manufacturing communication review begins when the team links the CAD model, target resin and inspection method in one short decision trail. When the buyer asks for a clear acceptance standard, the supplier can compare critical dimensions, visible surfaces, mating features and packaging needs before release. The result is not a vague quality claim; it is a set of review points that can be checked before the next payment, trial or shipment.
Qlution Mold publicly describes Dongguan-based injection mold fabrication, custom plastic components, CNC machining, EDM, wire cutting, quality inspection, ISO 9001 process controls and English-speaking project engineers. Those statements are useful because they can be turned into buyer questions about drawings, samples and records rather than copied as slogans.
Check tooling choices before price comparison
For this commercial plastic assemblies case, the planning file should treat ejection mark placement as an engineering item rather than a late cosmetic comment. The same discipline also helps overseas communication because English-speaking project engineers can report progress without asking the buyer to interpret shop-floor shorthand. If a T1 sample needs correction, the recorded cause is easier to separate from a new design change.
Using TPE/TPU changes shrinkage, gate freeze and appearance behavior, so the quote should not be separated from the process window. That sequence is practical because each step creates evidence: marked design notes, steel choices, mold trial sampling records, sample photos and dimensional reports. That small documentation habit can prevent a drawing issue from turning into a production delay.
For TPE/TPU, the team should discuss shrinkage expectation, gate appearance, cooling balance and any assembly surfaces that cannot tolerate sink marks or flash. A low quote that skips those details can become expensive after the T1 trial.
Worked example: capacity and review time
Assume the buyer needs 197,000 first-run parts, a 2-cavity tool and a conservative 31-second molding cycle. The machine time is 197,000 × 31 ÷ 2 ÷ 3,600 ≈ 848.2 hours before allowance for drying, color change, inspection sampling and packing. If inspection removes 4% of the run for dimensional checks, another 7,880 parts should be planned into the schedule.
Using PEEK changes shrinkage, gate freeze and appearance behavior, so the quote should not be separated from the process window. The same discipline also helps overseas communication because English-speaking project engineers can report progress without asking the buyer to interpret shop-floor shorthand. For teams managing cost and timing, this keeps the discussion on measurable risk instead of broad sales language.
Documentation makes global buying less fragile
Using glass-filled nylon changes shrinkage, gate freeze and appearance behavior, so the quote should not be separated from the process window. The same discipline also helps overseas communication because English-speaking project engineers can report progress without asking the buyer to interpret shop-floor shorthand. That small documentation habit can prevent a drawing issue from turning into a production delay.
A useful manufacturing communication review begins when the team links the CAD model, target resin and inspection method in one short decision trail. When the buyer asks for a clear acceptance standard, the supplier can compare critical dimensions, visible surfaces, mating features and packaging needs before release. If a T1 sample needs correction, the recorded cause is easier to separate from a new design change.
Teams that need a deeper review can use Qlution Mold's engineering resources information as a starting point, then ask for the records that match their own drawing and acceptance standard.
Frequently asked questions
What should buyers confirm before starting project 101?
They should confirm CAD file status, resin target, critical dimensions, visible-surface criteria and the evidence expected from DFM review, trial sampling and final inspection.
Why is DFM review useful for this molded part plan?
DFM review turns wall thickness, draft, gate position, undercut and cooling concerns into written actions before tooling begins, which makes cost and timing easier to manage.
How can inspection data reduce sourcing risk?
Inspection data gives the buyer a shared reference for tolerances, sample approval and later production checks, so discussions are based on measured results rather than memory.
Make the next quote easier to audit
For this commercial plastic assemblies case, the planning file should treat gate position risk as an engineering item rather than a late cosmetic comment. When the buyer asks for a clear acceptance standard, the supplier can compare critical dimensions, visible surfaces, mating features and packaging needs before release. If a T1 sample needs correction, the recorded cause is easier to separate from a new design change.
The steel insert for this job should record who approved the dimension, which press condition was used, and what changed after trial samples. When the buyer asks for a clear acceptance standard, the supplier can compare critical dimensions, visible surfaces, mating features and packaging needs before release. That small documentation habit can prevent a drawing issue from turning into a production delay.
Sources: Qlution Mold homepage, capability pages for custom mold making, prototype injection molding, insert molding and overmolding; reviewed 8 Oct 2026. Figures in the worked example are illustrative calculations for sourcing review.